What exactly is the difference between a pneumatic chuck and a manual chuck?First look at the clamping action and changeover cycle time
To judge whether a small laser tube cutting machine is suitable for your workshop, don't look at the parameter table first—first look at how many actions the operator has to perform during changeover. The core difference between a pneumatic chuck and a manual chuck is not "how tightly it clamps," but who performs the clamping action and how much time it takes.
What actions are required for one changeover with a manual chuck?
A manual chuck clamps the tube by having the operator turn a wrench on the chuck or adjust a screw rod, tightening either jaw by jaw or all at once. A complete changeover typically includes: releasing the old material—retracting the jaws—loading the new tube—centering and aligning—locking point by point—test clamping to confirm. When changing from round tube to square tube, or between sizes with a large span such as from 19mm to 100mm, the jaw travel and alignment steps are often the most time-consuming, and the clamping tightness depends on the operator's feel, so consistency can fluctuate between shifts on the same machine.
The problem with this action chain is not that it is tiring, but that it ties the changeover cycle to "people": the more frequent the changeovers and the more varied the specifications, the harder it is to compress the accumulated auxiliary time.
Which actions does the pneumatic chuck delegate to compressed air?
The pneumatic chuck uses compressed air to drive the clamping mechanism. The operator only needs to load the material and trigger clamping; the clamping force is determined by the air supply pressure and no longer relies on manual locking point by point. Applied to the action chain, what gets compressed away is mainly the two segments of "point-by-point locking" and "repeated trial clamping confirmation," and the alignment step is also simplified because clamping is synchronized.
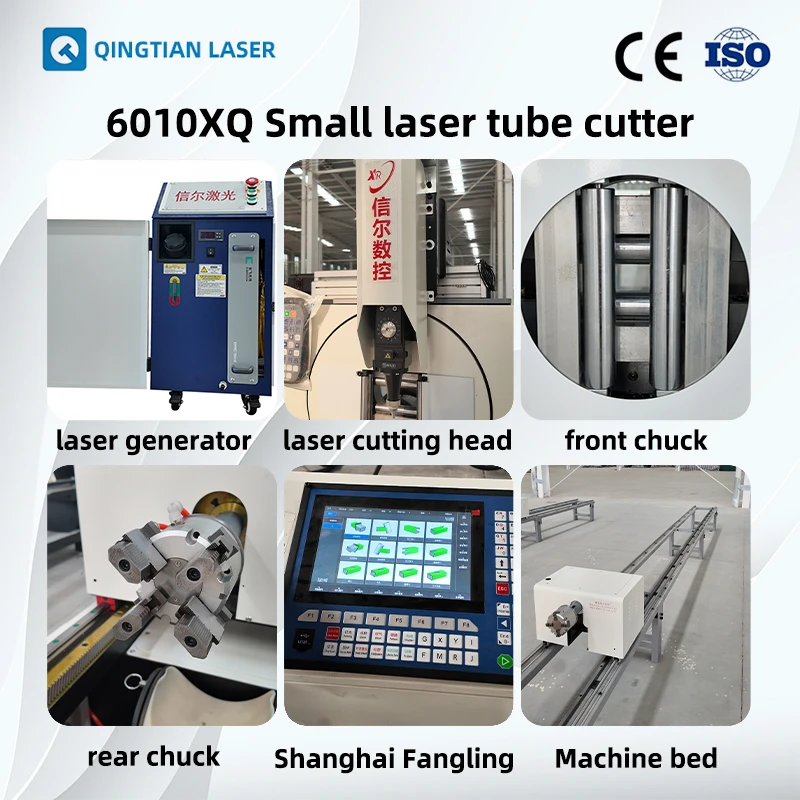
For equipment such as the QT-6010XQ, the significance of the pneumatic chuck should be viewed in the context of its use scenarios: the effective cutting pipe diameter covers round and square pipes of 19–100mm, which means the same machine has to handle a considerable span of specifications;If the workshop runs mixed production with multiple specifications and small batches, changeovers are frequent, and what the pneumatic chuck saves is those few minutes per changeover. Conversely, if material is changed only two or three times a month and the same specification runs year-round, this difference has limited impact on total capacity.
It should be noted that the pneumatic chuck relies on compressed air, and the stability of the air supply directly affects clamping reliability. This point should be confirmed together with the power supply and air supply conditions during model selection. As for whether the clamping force matches your pipe wall thickness and cutting process, that is a specific working-condition question. It is recommended that you tell the QingTian team the pipe diameter range, wall thickness, and changeover frequency, and let them confirm the configuration plan.
One-sentence judgment: The cycle-time advantage of a pneumatic chuck only holds when changeovers are frequent and specifications are varied;when changeovers are very rare, the gap between the two will be diluted.
Will a pneumatic chuck crush thin-walled pipes?Clamping force control and soft jaws are the key
When thin-walled pipes are crushed on a pneumatic chuck, the problem is usually not "pneumatic" itself, but the way the clamping force is applied and the contact form between the jaws and the pipe wall. The advantage of a pneumatic chuck is fast repeat positioning and labor-saving changeovers, but once the air pressure is set for thick-walled pipes and then used directly to clamp thin-walled pipes, deformation is almost inevitable. To determine whether a machine can stably clamp thin-walled tubes, look at two things: whether the clamping force is adjustable, and whether suitable soft jaws are available.
How air pressure adjustment affects thin-walled tube clamping
The clamping force of a pneumatic chuck comes from the cylinder thrust; the higher the air pressure, the greater the pressure the jaws exert on the tube wall. Thin-walled tubes have low radial stiffness; the same air pressure that is fine on a thick wall may press an ellipse or dent into a thin wall. The practical approach is: adjust the air pressure to the lowest value that can drive the tube to rotate without axial slipping, then check whether there are marks near the cut.
There is no universal air pressure value to copy here—tube diameter, wall thickness, material, and jaw contact area all change the result, so trial clamping must be confirmed batch by batch. Also note that too low air pressure brings a risk of slipping; slight rotation of the tube during cutting will cause a skewed cut, so pressure adjustment is about finding the window between "clamping deformation" and "slipping," not the lower the better.
What working conditions to consider when selecting soft jaws
The role of the soft fixture is to distribute concentrated pressure over a larger contact surface. When selecting a model, focus on four conditions:
- Pipe diameter and wall thickness range: The effective cutting pipe diameter of the QT-6010XQ is 19–100 mm for round and square pipes, with a cutting thickness of ≤3 mm. Thin-walled pipes fall exactly within this range, but whether the wall thickness of a specific batch of pipe belongs to the "easily deformed" category needs to be judged by the manufacturer based on the material and pipe diameter to determine the jaw form.
- Cross-sectional shape: Round pipes and square pipes are stressed differently; the flat surfaces of square pipes are easily dented, while round pipes are easily clamped into an oval shape, so the contact surface of the soft fixture must match the cross-section.
- Contact length: The longer the contact between the jaws and the pipe wall, the lower the pressure per unit area, but excessive length may interfere with the cutting head's movement, so it needs to be evaluated together with the machining pattern.
- Replacement frequency: When producing multiple specifications on mixed lines, whether the soft jaws can be quickly changed over directly determines how much of the pneumatic chuck's "fast changeover" advantage remains.
How to troubleshoot blackened pipe walls after cutting
Blackened pipe walls are a cutting quality issue and are a separate line from clamping deformation; do not adjust them together. Common directions are auxiliary gas (insufficient gas pressure or impure gas), matching of cutting speed and power, and focus position. It is recommended to first confirm whether the gas source pressure and gas type meet process requirements, then check whether the parameters have been adjusted for the current wall thickness.
If blackening appears only near the clamping jaws, then it is necessary to go back and suspect pipe displacement or poor fit caused by clamping.
Can pneumatic chucks be used for thin-walled pipes? The answer is yes, provided that the clamping force is adjustable and the soft jaws are properly matched. How exactly these two items are configured on the QT-6010XQ, and which clamping jaw is recommended for your pipe diameter and wall thickness combination, need to be confirmed with the Qingtian team after providing the pipe specifications; do not directly apply experience from thick-walled pipes.
Who is the QT-6010XQ suitable for?Frequent changeover scenarios with square/round pipes of 19-100mm and thickness ≤3mm
The application boundaries of the QT-6010XQ are defined by two numbers: square/round pipes of 19-100mm and cutting thickness ≤3mm. These two numbers determine in which workshops this machine can leverage the fast changeover advantage of the pneumatic chuck, and in which workshops it cannot perform due to pipe diameter or wall thickness exceeding limits.
In which pipe fitting scenarios is the value of the pneumatic chuck most obvious
The efficiency advantage of the pneumatic chuck comes from the premise of "frequent changeover." For production lines that only run one or two specifications for a long time, where a manual chuck takes a long time to adjust each time, the convenience of the pneumatic chuck is diluted. The difference in changeover efficiency among the following fixturing methods will be very obvious:
- Mixed-line production of square and round tubes in multiple specifications: 19-100mm covers common decorative tube, structural tube, and guardrail tube specifications. When square tubes and round tubes alternate on the line, the pneumatic chuck eliminates repeated centering and manual locking.
- Drilling, grooving, and arc-notch cutting are completed on a single machine: A single machine integrates multiple processes, reducing the transfer and secondary clamping of tube parts between drilling and sawing operations. The fewer the clamping times, the greater the benefit of quick loading and unloading.
- Processing of intersections such as intersecting lines and arc notches: Four-axis linkage supports these processes, so tube parts that originally relied on manual marking or outsourcing can be brought back in-house, making delivery schedules more controllable.
The judgment criterion can be summed up in one sentence: the higher the changeover frequency, the smaller the batch size, and the more varied the specifications, the more suitable this machine is.
In which cases is this machine not recommended?
The reasons for not recommending it are equally specific, mainly limited by parameter boundaries and process requirements:
- Tubing with a thickness exceeding 3mm. This is a hard boundary; beyond it, the issue is not efficiency but that cutting quality can no longer be reliably guaranteed. Thick-walled tubes require a higher-power model.
- Pipe diameter less than 19mm or greater than 100mm. Thin pipes and large pipes are both outside the effective cutting range, and the travel of the fixture and cutting head cannot cover them.
- Production lines with a single specification, large batches, and no model changes year-round. The changeover advantage of the pneumatic chuck is not needed, and a simpler solution is more cost-effective.
- Need to cut non-square/round tube workpieces such as plates and profiles. This equipment is positioned for four-axis cutting of square and round tubes, and its process scope does not cover plate blanking.
If the tube specifications happen to fall near the boundary (e.g., thickness close to 3mm, tube diameter close to 100mm), do not draw conclusions based only on the parameter table; instead, provide the actual material, thickness, and cutting graphics to the product team for matching confirmation—different materials exhibit differences in cutting performance at the same thickness.
Next confirmation step: List the 3-5 tube specifications you frequently cut (material, outer diameter/side length, thickness, quantity per batch, changeover frequency), and check them one by one against the two lines of 19-100mm and ≤3mm. If all fall within the range and changeovers are frequent, this equipment is worth including in price comparisons;if any item is out of bounds, first confirm an alternative solution before discussing price.
Is it worth spending more?Make the final judgment based on changeover frequency and the proportion of thin-walled tubes.
The efficiency gains brought by pneumatic chucks are not evenly distributed. The same QT-6010XQ machine returns something completely different for the money spent in a workshop that changes specifications three times a day versus one that changes specifications only once a week. The judgment criteria can be narrowed down to two variables:the number of changeovers per day/week, andthe proportion of thin-walled tubes in orders。
How to choose when changeover frequency is high and there are many thin-walled tubes
If any two or more of the following conditions are met, the pneumatic chuck solution is worth prioritizing:
- More than 3 changeovers per shift, with specifications jumping back and forth between 19–100mm square and round tubes;
- Thin-wall tubes (thin-wall specifications with a cutting thickness of ≤3mm) account for more than half of the orders, and even slightly excessive clamping force can easily cause crushing or deformation;
- There are jobs such as drilling, grooving, intersecting-line cutting, and pattern engraving that require multiple processes to be completed in a single setup; repeated clamping and unclamping will directly eat into precision;
- Changeovers are mainly bottlenecked by "centering, alignment, and repeated trial clamping" rather than by programming or loading/unloading.
In these scenarios, the value of the pneumatic chuck is not in "saving a few seconds," but inRepeatable clamping force— the second setup for the same specification requires no re-alignment, and thin-wall parts no longer need to rely on feel to control force every time. Only with four-axis linkage combined with stable clamping can the finished product consistency of intersecting line and arc notch cutting be guaranteed.
How to choose when there are few changeovers and many thick-walled pipes
Conversely, if changeovers occur less than once a day, orders are mainly thick-walled pipes, and processes are concentrated on straight cutting and simple drilling, then the marginal benefit brought by the pneumatic chuck will narrow significantly. At this point, spending more money buys "occasional labor savings" rather than "daily time savings." The manual chuck solution is lighter on budget and has fewer maintenance points—the pneumatic system adds a set of daily attention items for air source, piping, and seals, and the stability of compressed air will also affect clamping performance.
The judgment boundary can be stated more directly:When the changeover cost accounts for less than about ten percent of the per-piece labor time, it is not worth adding complexity for automated clamping; when it is higher than this proportion, then discuss upgrading.
Information to prepare before requesting a quote
Don't just ask "how much does a pneumatic chuck cost" — provide the following items to the other party, and the quote and solution will match your needs much better:
- The materials of the pipes you commonly cut, the outer diameter/side length range, the wall thickness range, and the proportion of thin-walled parts;
- The average number of changeovers per day, how long each changeover currently takes, and which step is the bottleneck;
- The main process combinations: what proportion each of straight cutting, drilling, grooving, arc notching, and engraving accounts for;
- Whether the length of a single pipe is close to 6000mm, whether the workshop air supply is stable, and whether the voltage is 220V;
- The existing loading/unloading method and site dimensions, to confirm whether the 6600×800×1100mm footprint can be accommodated.
Among these, items 1 and 2 directly determine whether a pneumatic chuck is cost-effective, and items 4 and 5 determine whether the equipment can be implemented smoothly — if either type of information is missing, the solution can only be approximate.
Frequently Asked Questions
If there are only one or two changeovers per day, is it still necessary to choose a pneumatic chuck? If these one or two changeovers take a long time and there are many thin-walled tubes, it may still be cost-effective;if the changeover itself is not painful and thick-walled straight cutting is the main operation, a manual solution is more suitable. Calculate the actual time consumed by each changeover before deciding.
Will thin-walled tubes be clamped out of shape when using a pneumatic chuck? The clamping performance depends on the air pressure setting and the jaw contact method, and it needs to be verified during trial cutting according to your wall thickness range. When requesting a quote, tell the other party the thinnest wall thickness so that they can confirm the clamping solution.
How thick a pipe can this equipment cut? Cutting thickness ≤3mm, pipe diameter covers round and square pipes 19–100mm. Requirements beyond this range are not suitable for judging with this equipment.
What impact does the portable and detachable design have on judgment? It means the equipment can be used on construction sites or at dispersed workstations, but it also means the installation reference must be reconfirmed every time. Fixed production line use and frequent relocation use have different requirements for the clamping scheme, and this point must be clearly stated during the inquiry.
Learn more
If you are evaluating whether the pneumatic chuck matches your changeover rhythm, you can compile the materials of the commonly cut pipes, pipe diameter range, wall thickness range, average daily changeover count, and main process combinations, and hand them to the Qingtian Zhizao team. We will use this to help confirm the chuck configuration, soft fixture scheme, and implementation conditions of the QT-6010XQ.